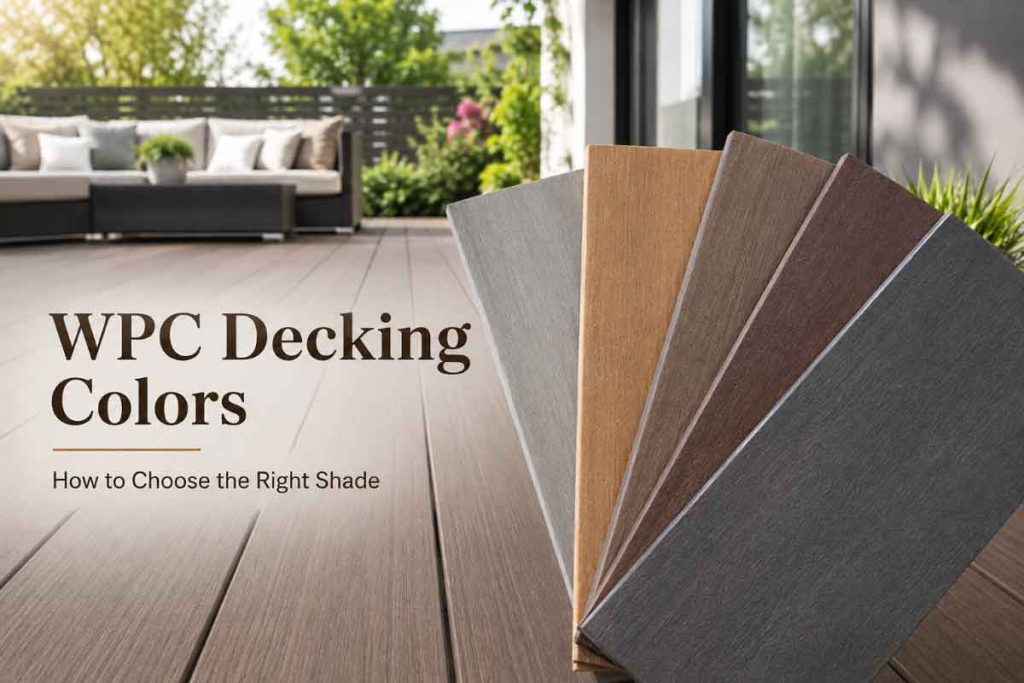
Color consistency is one of the most important quality concerns in WPC production, especially for large projects, repeat orders, and products installed side by side.
A buyer may order teak, coffee, light gray, silver gray, or charcoal WPC products several times. However, using the same color name does not automatically guarantee that every production batch will look exactly the same.
WPC products contain wood fibers, plastic materials, pigments, additives, and processing agents. Changes in any of these materials or in the extrusion process may affect the final appearance.
Surface texture, lighting, temperature, production speed, and co-extrusion layers can also influence how the color is seen.
Therefore, a professional WPC factory needs a controlled system for formulas, materials, production settings, reference samples, batch identification, and inspection.
Why Can WPC Colors Vary Between Batches?
WPC color is created by several factors working together.
These factors may include:
- Wood-fiber color
- Wood-fiber moisture
- Plastic material
- Pigment type
- Pigment quantity
- Additives
- Mixing consistency
- Extrusion temperature
- Production speed
- Cooling conditions
- Surface treatment
- Protective co-extrusion layer
Even when the same pigment formula is used, a change in the base materials may affect the final color.
For example, a slightly darker wood-fiber batch may make the finished board appear warmer or deeper. Different moisture levels may also affect material flow and surface appearance during extrusion.
As a result, color consistency depends on the complete production process rather than pigment alone.
Does the Factory Use an Approved Color Sample?
An approved physical sample is one of the most important references for batch color control.
The sample may be used to confirm:
- Color tone
- Surface treatment
- Embossing pattern
- Gloss level
- Product profile
- General appearance
The factory should label the approved sample clearly with information such as:
- Product code
- Color name or code
- Surface pattern
- Customer or project reference
- Sample version
- Approval date
- Order number
This prevents the production team from comparing the new batch with an outdated or unapproved sample.
Digital photos should not replace a physical color sample because cameras, screens, lighting, and image compression can change how the color appears.
How Are Color Formulas Recorded?
The factory should connect every approved color with a recorded pigment formula.
A color formula may include:
- Pigment type
- Pigment code
- Pigment quantity
- Base-material quantity
- Additive ratio
- Mixing sequence
- Mixing time
- Product formula
- Co-extrusion surface formula
Workers should follow the approved formula instead of adjusting the color only by visual judgment.
Accurate weighing is especially important because small changes in pigment ratio may become visible across a large production quantity.
The factory may also record the supplier and batch number of the pigment so that repeat orders can be traced more easily.
Why Must Raw Materials Be Controlled?
The same color formula may produce different results when the raw materials change.
WPC production commonly uses:
- Wood fibers
- Polyethylene or another plastic material
- Color pigments
- Coupling agents
- Lubricants
- Stabilizers
- Processing additives
The factory should control the source, quality, moisture, cleanliness, and batch identity of these materials.
If a repeat order requires close color matching, the factory may try to use materials with specifications similar to the previous order.
However, raw materials cannot always remain completely identical over long periods.
For this reason, the retained sample and recorded production data should be used together when preparing the new batch.
How Does Wood-Fiber Moisture Affect Color?
Wood fibers must be prepared carefully before mixing and extrusion.
If the moisture level is too high or unstable, it may affect:
- Material mixing
- Extrusion stability
- Surface texture
- Color appearance
- Product density
- Visible marks
Moisture may also create an uneven or cloudy surface appearance.
Therefore, the factory should control wood-fiber drying and storage conditions before production.
The material should be protected from rain, high humidity, and obvious contamination.
Consistent moisture control helps improve both color stability and extrusion quality.
How Are Pigments Weighed and Mixed?
Pigments should be measured according to the approved formula.
The factory may use weighing equipment to control the required quantity for each material batch.
After weighing, the pigment must be distributed evenly throughout the mixture.
Poor mixing can create:
- Dark or light streaks
- Local color spots
- Uneven board surfaces
- Differences between the beginning and end of a batch
- Inconsistent color between boards
The factory should therefore control:
- Mixing sequence
- Mixing time
- Batch quantity
- Equipment cleanliness
- Material temperature
- Material transfer
Different color batches should remain clearly identified throughout mixing and production.
Why Is Equipment Cleaning Important?
Material from the previous order may remain inside mixers, feeders, extruders, or transfer equipment.
If the previous product used another color, the remaining material may affect the new batch.
This is especially important when changing:
- From dark to light colors
- From charcoal to gray
- From coffee to teak
- From standard WPC to a pale co-extrusion surface
The factory may need to clean the equipment or run transitional material before producing qualified boards.
The first boards after a color change should be separated and inspected carefully.
They should not be included in the finished order until the color becomes stable.
How Does Extrusion Temperature Affect Color?
WPC materials are heated during extrusion.
Temperature influences material flow, surface formation, and color appearance.
If the temperature is too high or unstable, it may cause:
- Darker surfaces
- Burn marks
- Uneven color
- Surface degradation
- Inconsistent gloss
If the temperature is too low, material flow and surface quality may become unstable.
The factory should record the suitable temperature range for each product formula and profile.
During repeat production, technicians can refer to the previous settings and then make controlled adjustments when necessary.
Why Does Production Speed Matter?
Extrusion speed and pulling speed affect how long the material remains inside the equipment and how the profile cools.
Changes in speed may influence:
- Surface appearance
- Embossing depth
- Gloss
- Color tone
- Product dimensions
- Cooling stability
For example, a slower production speed may expose the material to heat for a longer time. This may slightly change the surface appearance.
Therefore, factories should avoid unnecessary speed changes during one batch.
When production settings must be adjusted, the first boards after the adjustment should be checked again.
How Does Surface Treatment Change the Visible Color?
The same WPC material may look different after brushing, sanding, grooving, or embossing.
A brushed surface may appear lighter because it reflects light differently. A deeply embossed surface may appear darker because shadows form inside the wood-grain pattern.
Surface appearance may also be affected by:
- Brush strength
- Sanding level
- Embossing pressure
- Roller temperature
- Pattern depth
- Production speed
- Surface direction
Therefore, color approval should include the final surface treatment.
A smooth color sample should not be used as the only reference for a deeply embossed product.
Why Can Co-Extrusion Colors Be More Complicated?
Co-extrusion WPC products contain a core and an outer protective layer.
The visible color mainly comes from the outer layer rather than the core.
The factory must control:
- Surface-layer pigment
- Surface-layer thickness
- Coverage consistency
- Bonding
- Pattern distribution
- Cooling conditions
- Core and layer compatibility
If the protective layer becomes too thin or uneven, the product may show visible color differences.
Some co-extrusion products also use multi-tone wood-grain effects. In this case, the pattern position may vary naturally from board to board.
The factory should control the overall color family and pattern quality rather than expecting every printed or mixed grain line to appear in exactly the same position.
How Is the First Board Compared With the Sample?
Before continuous production begins, the factory should inspect the first qualified boards.
The comparison may include:
- Main color tone
- Warm or cool appearance
- Lightness or darkness
- Surface pattern
- Embossing depth
- Gloss
- Profile dimensions
- Product weight
The board should be compared with the approved sample under reasonably consistent lighting.
If the first board is outside the approved range, the factory may adjust:
- Pigment ratio
- Mixing
- Extrusion temperature
- Production speed
- Surface-treatment settings
- Co-extrusion layer
Mass production should continue only after the color becomes acceptable and stable.
How Is Color Checked During Mass Production?
Color should not be checked only at the beginning of the order.
During a long production run, changes may occur because of:
- New material batches
- Pigment replenishment
- Shift changes
- Equipment adjustments
- Temperature changes
- Production interruptions
Quality-control staff should inspect boards at regular intervals.
They may compare selected boards with:
- The approved sample
- The first qualified board
- The specification sheet
- The previous inspection result
Boards with obvious differences should be separated for further evaluation.
Regular inspection helps the factory identify a color shift before a large quantity is produced.
How Are Different Material Batches Managed?
Large orders may require several raw-material and pigment batches.
The factory should record which materials were used in each production period.
Batch records may include:
- Production date
- Production line
- Material batch
- Pigment batch
- Product code
- Color code
- Mold number
- Shift
- Qualified quantity
If a color problem appears, the factory can use these records to identify the affected products.
Clear batch management also helps prevent visibly different boards from being mixed randomly during packaging.
Should Different Batches Be Packed Separately?
When a large order is produced in several batches, the factory may pack and label the batches separately.
Labels may include:
- Product code
- Color
- Production batch
- Board length
- Quantity
- Bundle number
- Order number
This makes the products easier to trace after delivery.
For projects where appearance is especially important, installers may use boards from the same batch in one continuous area.
This can reduce the visual effect of small acceptable differences between batches.
The buyer should communicate this requirement before packaging begins.
How Does Lighting Affect Color Inspection?
Color can appear different under:
- Factory lights
- Natural daylight
- Direct sunlight
- Shade
- Warm indoor lighting
- Cool indoor lighting
Phone cameras and computer screens can also change the visible result.
Therefore, the factory should use a consistent inspection location and lighting condition whenever possible.
For important color approvals, the buyer should rely on physical samples rather than video alone.
Video inspections can still help review the factory’s comparison process, but they are not the most accurate method for final color approval.
What Is an Acceptable Color Tolerance?
WPC is not a painted metal or printed paper product. It contains wood fibers and is produced continuously.
Therefore, very small color differences may occur.
The factory and buyer should agree on what level of difference is acceptable.
The acceptable range may depend on:
- Product type
- Surface texture
- Project size
- Installation location
- Color
- Co-extrusion pattern
- Buyer requirements
The goal is to maintain a consistent overall appearance without promising that every board will be completely identical under every lighting condition.
Clear expectations help reduce disputes after delivery.
What Happens When a Batch Is Outside the Approved Color Range?
Boards with an obvious color difference should be separated from qualified goods.
The factory may then:
- Review the pigment formula
- Check the raw-material batch
- Inspect mixing records
- Check equipment cleanliness
- Review extrusion settings
- Compare surface treatment
- Adjust the production process
- Produce replacement quantities
The affected boards should not be mixed into the customer’s order without approval.
Depending on the factory’s procedures, they may be reclassified, recovered through a controlled process, or handled separately.
How Are Repeat Orders Matched to Previous Batches?
For repeat orders, the factory should review the retained sample and previous production records.
These records may include:
- Approved sample
- Color formula
- Pigment batch information
- Material formula
- Mold number
- Extrusion settings
- Surface-treatment settings
- Production date
- Inspection results
- Packaging records
Before mass production, the factory may prepare a new pre-production sample or first-board comparison.
This is especially important when the previous order was produced several months or years earlier.
Even with detailed records, raw-material batches and pigment supply may change over time.
Therefore, buyers should not expect an old digital photo to provide an exact color standard for a new order.
Can Decking, Fencing, and Wall Panels Use the Same Color?
Different WPC products may use similar color names, but their final appearance may not match exactly.
The difference may come from:
- Different formulas
- Different molds
- Different surfaces
- Different embossing patterns
- Different protective layers
- Different production lines
For example, gray decking with deep embossing may appear darker than a smooth gray fence panel.
When several product types will be installed together, the buyer should request samples of each product category.
The factory can then confirm whether they can match closely or only remain within the same general color family.
What Should Buyers Confirm Before Production?
Buyers can help improve batch consistency by confirming:
- Final color sample
- Product profile
- Surface treatment
- Embossing pattern
- Standard or co-extrusion structure
- Acceptable color tolerance
- Product categories that must match
- Packaging and batch-label requirements
- Repeat-order reference
- Project installation areas
Buyers should also avoid changing the color after pigments and materials have already been prepared.
Late changes may require new samples, cleaning, material adjustments, and production rescheduling.
What Should Buyers Check Before Shipment?
Before shipment, buyers may review:
- Sample comparison photos
- Batch labels
- Finished-product photos
- Color consistency across bundles
- Product codes
- Packing list
- Final inspection results
- Packaging identification
For large or color-sensitive projects, the buyer may arrange a pre-shipment inspection.
The inspection should compare randomly selected boards from different bundles and production batches.
However, the approved physical sample should remain the main color reference.
Final Thoughts
Keeping WPC colors consistent between production batches requires control at every stage.
The factory must manage raw materials, wood-fiber moisture, pigment formulas, weighing, mixing, equipment cleaning, extrusion temperature, production speed, cooling, surface treatment, and co-extrusion layers.
An approved physical sample provides the main visual reference, while formulas, batch records, production settings, and regular inspections support repeatability.
Minor acceptable variations may still occur because WPC contains natural wood fibers and is produced through a continuous extrusion process.
For importers, distributors, contractors, and project buyers, confirming realistic tolerances and clear batch-label requirements can help reduce color-related risks.
At Senlai, approved color samples are linked with production formulas, material batches, surface requirements, and inspection records. Our team compares the first production boards with the approved reference and checks color consistency during production, packaging, and final inspection.